
Precision Engineering for Maximum Efficiency
- Maximize Yields: Achieve up to 98%+ solvent recovery rates, preventing costly raw materials from venting into the atmosphere.
- Column Pressure Stability: Maintain tight pressure control across varying vapor loads to keep your distillation column operating in its sweet spot.
- Minimized Vent Losses: Drastically reduce non-condensable vapor carryover to protect downstream vacuum equipment and comply with strict emission targets.
- Corrosion Resistance: Built to handle aggressive process streams, including alcohols, ketones, and organic solvents, without degradation.
Every solvent recovery condenser we build at GYRO is tailored to reduce overall energy consumption. Whether you are replacing a legacy unit or building out a new distillation skid, our designs integrate directly into your existing footprint while optimizing cooling utility usage.
Working Mechanics of Our Recovery Tower Condenser

Rapid Vapor-to-Liquid Phase Transformation
- Targeted Thermal Exchange: Chilled water, glycol, or cooling media flows through a multi-pass tube heat exchanger circuit to pull latent heat out of the vapor instantly.
- Instant Liquefaction: Vapor rapidly condenses on cold tube surfaces, forming a continuous liquid film that drains efficiently into the collection manifold.
Multi-Stage Condensation & Secondary Sub-Cooling
- Primary Overhead Condensing: Converts the bulk vapor volume into liquid reflux immediately upon entry.
- Integrated Secondary Vent Sub-Cooler: A dedicated sub-cooling section chills remaining non-condensable gas streams below ambient temperatures, trapping volatile light ends and preventing vent vapor carryover.

Process Efficiency & Thermodynamic Metrics
|
Condensing Stage |
Physical Mechanism |
Operational Advantage |
|
Primary Knockdown |
Saturated vapors pass over main cooling tube bundles |
Rapidly converts over 95% of incoming overhead vapors |
|
Secondary Sub-Cooling |
Non-condensables route through a dedicated secondary process vapor sub-cooler |
Minimizes solvent vent loss and reduces emissions |
|
Reflux Discharge |
Condensed liquid drains under low vapor pressure drop |
Ensures stable liquid reflux ratios and column hydraulic balance |
Thermodynamic Optimization for Column Stability
- Zero Backpressure Build-Up: Protects upstream distillation columns from pressure surges and vacuum collapse.
- Controlled Vapor Velocity: Maximizes overall heat transfer coefficients while eliminating tube vibration and liquid entrainment.
- Stable Reflux Ratios: Delivers steady liquid return to the column top, maintaining constant vapor-liquid equilibrium throughout production runs.
Recovery Tower Condenser Engineering Highlights
20+ Years of Process Metallurgy Expertise
Our technicians bring over two decades of practical process heat transfer experience to every build. We combine precision shell fit-up with automated welding techniques to ensure structural integrity across high-vacuum and high-pressure duties.
Advanced Materials for Solvent Streams
GYRO manufactures every stainless steel distillation condenser using advanced alloys specifically designed for your chemical media, preventing stress corrosion cracking and shell erosion.
|
Material Option |
Ideal Solvent Application |
Core Advantage |
|
SUS304 / SUS304L |
Ethanol, general alcohol recovery |
Cost-effective standard corrosion resistance |
|
SUS316 / SUS316L |
Methanol, acetone, IPA streams |
Superior pitting resistance in organic vapors |
|
Titanium & Hastelloy |
DMF, acidic organic solvents, halides |
Maximum corrosion immunity in harsh process media |
|
Anti-Corrosion Coatings |
Specialized chemical vapors |
Extended shell and bundle protection |
Total Traceability and Defect-Free Testing
- 100% Heat Number Traceability: Full Material Test Reports (MTRs) and heat numbers tracked across all shell plates, tubesheets, tubes, and flanges.
- Multi-Stage Leak Testing: Every shell and tube vapor condenser undergoes rigorous hydrostatic, pneumatic, and helium leak detection before dispatch.
- Flange Performance Guarantee: Backed by our direct replacement guarantee on critical flange assemblies to eliminate initial startup leaks.
Tailored Tube Bundle Arrangements
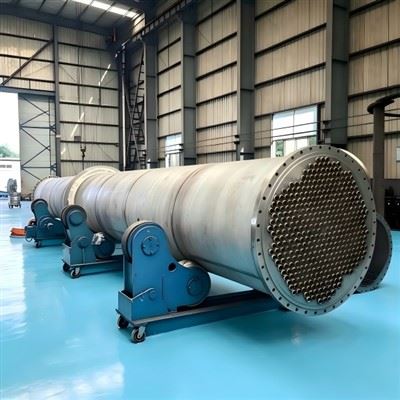
- Fixed Tubesheet: Compact, leak-tight design best suited for clean vapor condensation.
- U-Tube Bundle: Allows independent thermal expansion between shell and tubes to prevent joint fatigue.
- Floating Head: Fully removable bundle configuration engineered for heavy fouling streams requiring quick mechanical cleaning.
Technical Specifications: Recovery Tower Condenser
We engineer every recovery tower condenser to match your exact process duty, vapor loads, and system hydraulics.
|
Parameter |
Operating Range & Design Capabilities |
|
Heat Transfer Area |
5 m² to 500 m²+ (Custom-sized to column overhead duty) |
|
Operating Pressure |
Full Vacuum (-0.1 MPa) up to 2.5 MPa |
|
Design Temperature |
-20°C to 250°C |
|
Primary Materials |
SUS304, SUS316L, Duplex Stainless Steel, Carbon Steel (Shell) |
|
Orientation Types |
Vertical, Horizontal, or Inclined Overhead Condensers |
|
Design Standards |
ASME Sec VIII Div 1, GB150, PED Compliant |
|
Cooling Media |
Cooling tower water, chilled glycol, process brine, cold condensate |
Flexible Integration & Code Compliance
- Targeted Metallurgy: We select process-wetted alloys tailored to your vapor streams to prevent pitting, cracking, and early tube failure.
- Versatile Utility Compatibility: Engineered to run smoothly on standard cooling tower loops, sub-zero chilled glycol, or cold process condensate streams.
- Global Standard Stamping: Built and certified strictly to ASME, PED, or GB150 codes for smooth compliance and rapid site integration globally.
Industrial Applications for Your Recovery Tower Condenser
We engineer our recovery tower condenser systems to perform across high-stakes chemical, pharmaceutical, and processing environments. Whether you need an overhead distillation condenser for continuous fractionation or a secondary vent vapor recovery condenser for strict emission standards, our equipment delivers precise thermal energy exchange and maximum solvent recovery yields.
Heavy-Duty Solvent Processing Capabilities
|
Industry Sector |
Application Focus |
Target Solvents & Vapors |
|
Pharmaceutical & Chemical |
Extraction tower vapor recovery |
Ethanol, Methanol, Isopropanol (IPA), Ethyl Acetate, Methylene Chloride |
|
Distillation & Rectification |
Overhead reflux condensation |
High-purity alcohol streams, fractionated hydrocarbons, stripping column overheads |
|
VOC & Emission Control |
Vent vapor capture |
Storage tank emissions, reactor exhausts (Zero-discharge targets) |
|
Petrochemical Processing |
High-pressure hydrocarbon recovery |
Light hydrocarbon vapors, hot process condensate |
Primary Deployment Scenarios
- Pharmaceutical & Chemical Solvent Recovery: Configured as a corrosion-resistant solvent recovery condenser, handling aggressive mixed solvent streams directly from extraction units without vapor blow-by.
- Distillation & Rectification Columns: Functions as a dedicated alcohol recovery tower heat exchanger or methanol rectifying condenser, maintaining consistent liquid reflux ratios to stabilize column operating pressure.
- VOC & Vent Vapor Capture: Serves as a high-efficiency process vapor condenser placed on reactor vents and tank exhausts to capture volatile organic emissions before they leave the loop.
- Petrochemical Duty: Engineered to withstand elevated system pressures and thermal cycling while continuously recovering light hydrocarbon vapors into high-purity process condensate.


Custom Recovery Tower Condenser Options
GYRO provides skid-mounted systems with pre-wired electrical connections, pre-installed piping, and factory testing, fully customized to meet your specific process requirements.
Fully Integrated Package: High-efficiency process steam condensers and reboilers, buffer tanks, reflux pumps, control valves, and instrumentation are integrated into a compact skid-mounted unit.
Plug-and-Play Installation: Factory assembly and testing significantly reduce on-site installation time, minimize field work, and lower commissioning risks.
Customized Port Orientation: Flanges are aligned to perfectly match your existing distillation column piping. Compact Footprint: Designed for tight mechanical spaces, eliminating the need to modify existing structural supports.
Feed Preheating: An optional heat recovery loop utilizes heat from the overhead condenser vapors to preheat the feed stream entering the column.
Reduction of Vapor Load: Reduces the total boiler load, lowers operating costs, and improves the overall thermal efficiency of the entire plant.
If you are interested in our recovery tower condenser, please contact us immediately; GYRO will develop a suitable solution based on your requirements and operating conditions.
Hot Tags: recovery tower condenser, China recovery tower condenser manufacturers, suppliers, factory, Acid Gas Preheater, Exhaust Gas Heat Exchanger, heat exchanger, Industrial Heat Exchangers, Shell and Tube Heat Exchanger, U Tube Heat Exchanger